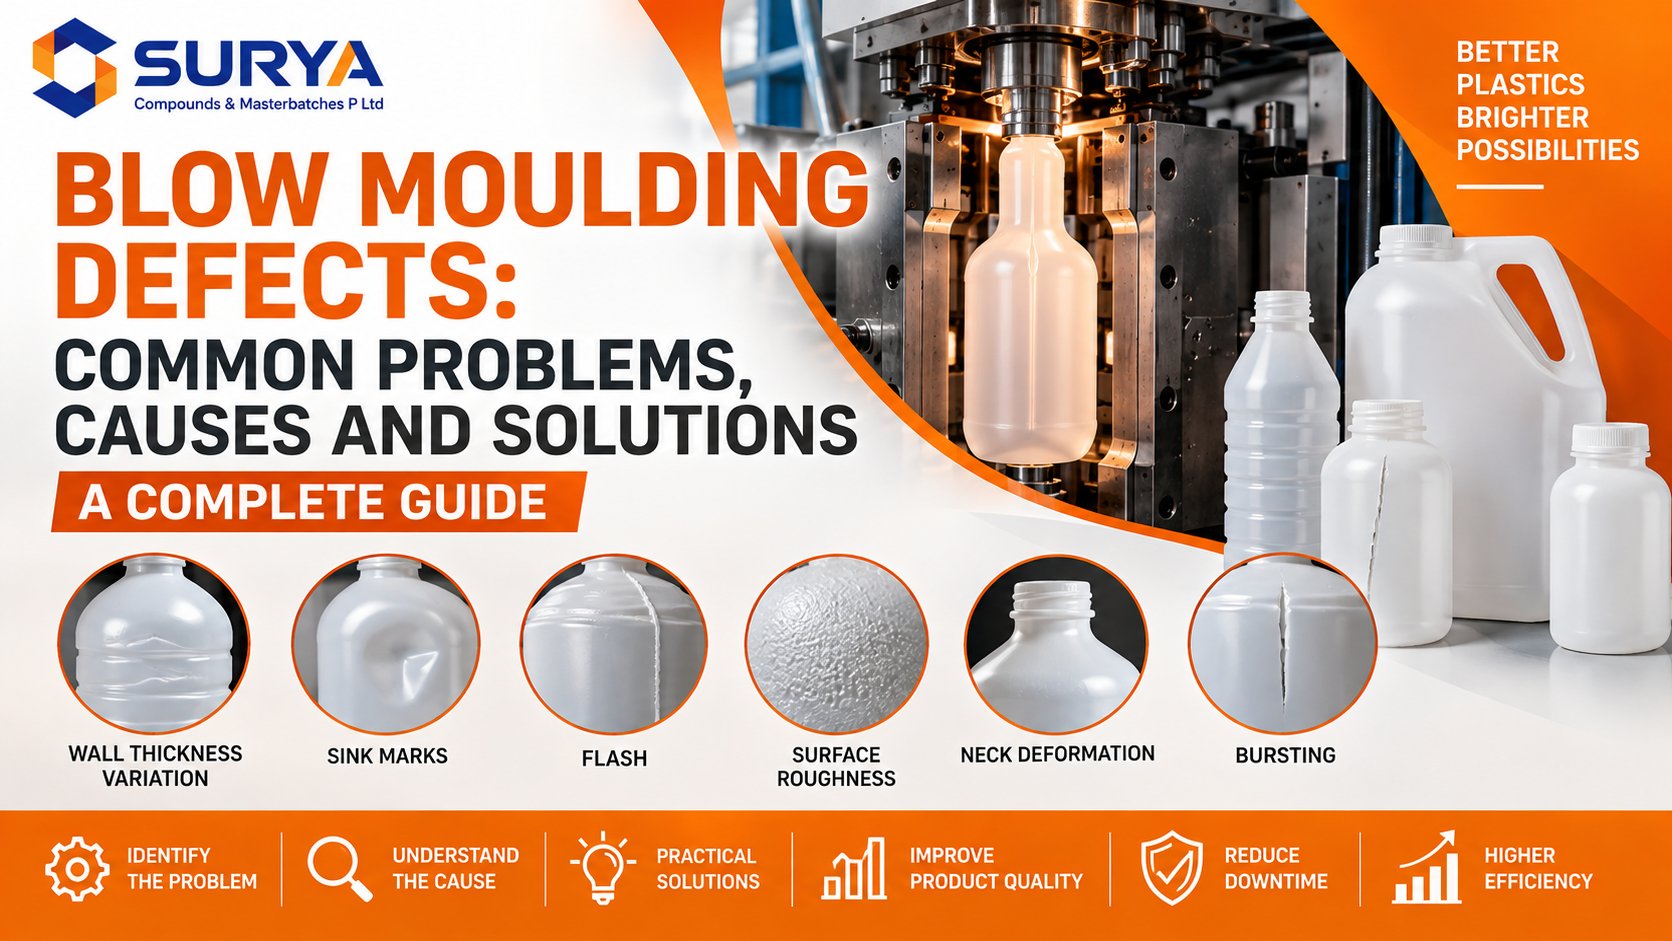
Blow moulding defects can reduce product quality, increase scrap rates, slow production, and create problems during leak, dimensional, or performance testing. Common issues include uneven wall thickness, parison sagging, excessive flash, poor surface finish, bubbles, black specks, blow-outs, weak pinch-off, warpage, and incomplete blowing.
Most blow moulding problems are linked to one or more factors involving the raw material, melt temperature, parison, mould, blowing air, cooling system, machine settings, or masterbatch selection. A structured troubleshooting process helps identify the root cause before changing multiple parameters at once.
This guide explains the most common blow moulding defects, their causes, and practical solutions. It also covers how material selection, MFI, masterbatch compatibility, and processing conditions affect blow-molded products.
Quick Answer: What Are the Most Common Blow Moulding Defects?
The most common blow moulding defects include:
- Uneven wall thickness
- Parison sagging or drawdown
- Parison curling
- Excessive flash
- Weak pinch-off
- Blow-outs or parison rupture
- Incomplete blowing
- Bubbles and voids
- Black specks and contamination
- Die lines and streaks
- Rough or dull surface
- Poor mould definition
- Warpage and dimensional variation
- Bottom defects
- Neck deformation
- Leakage
- Colour variation
- Poor masterbatch dispersion
The correct solution depends on where the defect originates. The same visible problem can have different causes, so processors should examine the material, parison, machine, mould, air supply, and cooling system before making process changes.
Blow Moulding Defects and Solutions at a Glance
|
Defect |
Common Causes |
Possible Solutions |
|
Uneven wall thickness |
Incorrect parison profile, die misalignment, uneven temperature | Adjust parison programming, centre die, check temperature zones |
|
Parison sagging |
Excessive melt temperature, low melt strength, long open time |
Optimise melt temperature, reduce delay, review resin grade |
|
Parison curling |
Die alignment issue, uneven heating, low melt temperature |
Check the centring, tooling, and temperature. |
|
Excessive flash |
Oversized partition, mould alignment, excessive material |
Check parison size, mould closure and pinch-off |
|
Weak pinch-off |
Incorrect pinch-off geometry, cold or thin partition |
Check pinch-off and material distribution. |
|
Blow-out |
Thin partition section, excessive blow pressure, poor pinch-off |
Improve wall distribution and review blow pressure. |
|
Bubbles |
Moisture, trapped air, contamination |
Check material handling, drying requirements, and venting. |
|
Black specks |
Degraded resin, contamination, excessive residence time |
Clean equipment and investigate material source. |
|
Die lines |
Dirty/damaged die, contamination, unstable flow |
Inspect die lip and melt flow |
| Rough surface | Poor venting, incorrect temperature, moisture, low air pressure |
Check mould vents, melt temperature and air pressure |
|
Incomplete blowing |
Insufficient air, blocked blow pin, poor venting | Check air delivery, blow pin and mould vents |
|
Warpage |
Uneven cooling, early ejection, uneven wall thickness | Balance cooling and review wall distribution |
| Colour variation | Poor dispersion, incorrect dosage, incompatible carrier |
Verify masterbatch compatibility and dosage |
| Leakage | Thin wall, weak pinch-off, pinholes, trimming damage |
Locate leak and trace it to the forming stage |
1. Uneven Wall Thickness
Uneven wall thickness is one of the most common blow moulding defects. It occurs when material does not distribute evenly across the mould cavity.
A finished bottle, container, tank, or hollow component might have thick areas in one section and extremely thin areas in another.
Common causes
- Incorrect parison thickness profile
- Die not properly centred
- Uneven die-head temperature
- Parison sagging
- Incorrect mould positioning
- Excessive stretching during blowing
- Incorrect resin melt strength
- Inconsistent extrusion
- Improper mould design
Solutions
Start by checking the parison before it enters the mould.
Then:
- Check die and mandrel alignment.
- Review the parison programming profile.
- Verify temperature across the die head.
- Check extrusion stability.
- Review resin MFI and melt strength.
- Inspect mould alignment.
- Measure wall thickness at multiple points.
Material selection also matters. Blow moulding generally benefits from suitable melt strength and controlled flow behaviour. Surya Compounds & Masterbatches explains the relationship between MFI, flow behaviour, melt strength, and polymer processing in its guide on Melt Flow Index in Plastics.
2. Parison Sagging or Drawdown
Parison sagging occurs when the hot extruded tube stretches downward under its own weight before the mould closes.
This can create:
- Uneven wall thickness
- Thin sections
- Poor bottom formation
- Incorrect part weight
- Inconsistent dimensions
Causes of parison sagging
- Melt temperature is too high
- Resin has insufficient melt strength
- Excessive time between extrusion and mould closing
- Extrusion speed is too low
- Incorrect material grade
- Excessive parison length
Blow moulding troubleshooting
Check the parison immediately after extrusion.
If the parison becomes excessively long or thin before mould closure:
- Check melt temperature.
- Review extrusion speed.
- Reduce unnecessary delay before mould closing.
- Review resin grade and melt strength.
- Check die-head temperature uniformity.
Do not make large temperature changes without considering the resin manufacturer’s recommended processing window.
3. Parison Curling
Parison curling occurs when the extruded tube bends or moves away from the desired position.
This creates problems during mould closing and affects material distribution.
Possible causes
- Die and mandrel misalignment
- Uneven temperature around the die
- Incorrect die-head setup
- Poor melt flow
- Low melt temperature
- Uneven material flow
Solutions
- Centre the die and mandrel.
- Check die-head temperature zones.
- Inspect the die lip.
- Check for contamination inside the flow path.
- Verify stable extrusion.
- Confirm that the selected resin is suitable for the application.
Parison curling and drawdown are established troubleshooting categories in blow moulding process guides.
4. Excessive Flash
Flash is excess plastic that forms outside the intended product area, particularly around the parting line and pinch-off.
Some flash is expected in extrusion blow moulding and is removed during trimming. Excessive or inconsistent flash indicates a process, tooling, or material distribution problem.
Common causes
- Parison is too large
- Incorrect mould closing
- Poor mould alignment
- Damaged pinch-off area
- Excessive material
- Insufficient clamping
- Incorrect parison placement
Solutions
Check:
- Parison diameter
- Parison thickness
- Mould alignment
- Clamp operation
- Pinch-off condition
- Part weight
- Tooling wear
Do not automatically reduce overall material weight. A reduction might create thin walls elsewhere.
5. Weak Pinch-Off or Bottom Failure
The pinch-off creates the welded area in many extrusion blow moulded products. A weak pinch-off can lead to leaks, cracks, and product failure.
Causes
- Insufficient material at the pinch area
- Incorrect pinch-off geometry
- Poor parison positioning
- Contaminated material
- Incorrect temperature
- Excessive trimming
- Tool wear
Solutions
Inspect the failed area first.
Look for:
- Thin weld line
- Torn weld
- Contamination
- Uneven material distribution
- Sharp or damaged pinch-off edges
If the problem is repeated, inspect the mould and pinch-off tooling rather than changing the entire process recipe.
6. Blow-Out or Parison Rupture
A blow-out occurs when the parison breaks during inflation.
It usually appears as a burst or open section in the finished product.
Common causes
- Excessive blow pressure
- Excessive blow-up ratio
- Thin parison section
- Weak material distribution
- Poor pinch-off
- Incorrect mould closing
- Low melt strength
Solutions
- Identify exactly where the parison breaks.
- Check wall thickness around the failure.
- Review blow pressure.
- Check parison programming.
- Inspect pinch-off geometry.
- Review resin melt strength.
- Check whether the failure follows a specific mould cavity.
A thin section should be corrected at its source rather than compensating by increasing material across the entire part.
7. Bubbles and Voids
Bubbles can appear inside or on the surface of blow moulded products.
Moisture, trapped air, contamination, and material degradation are common areas to investigate. Industry troubleshooting references also identify moisture and contamination as potential causes of bubbles, streaks, and surface problems.
Possible causes
- Moisture or condensation
- Improper material storage
- Contamination
- Air entrapment
- Material degradation
- Poor mixing
- Inconsistent extrusion
Solutions
- Follow the resin supplier’s material-handling requirements.
- Check storage conditions.
- Inspect the hopper and feed system.
- Check regrind quality.
- Inspect the extruder and die head.
- Look for degraded material.
- Check mould venting.
Do not assume every polymer requires the same drying procedure. Follow the requirements for the specific resin.
8. Black Specks and Burn Marks
Black specks are a serious quality issue in bottles, containers, packaging products, and other blow moulded components.
Common causes
- Degraded polymer
- Contaminated regrind
- Foreign material
- Excessive residence time
- Overheating
- Poor machine cleaning
- Material trapped inside the die or extruder
Blow moulding problems and solutions
First determine whether the black specks are random or appear repeatedly in the same position.
If they occur at a fixed location, inspect the corresponding flow path.
If they appear randomly, investigate:
- Resin lot
- Regrind
- Hopper
- Feeding system
- Purging history
- Start-up and shutdown procedures
Use the machine manufacturer’s recommended cleaning and purging procedure.
9. Die Lines and Streaks
Die lines appear as continuous lines or marks on the finished product.
They often follow a fixed position around the part.
Possible causes
- Damaged die lip
- Contamination
- Degraded polymer
- Material buildup
- Unstable melt flow
- Poor dispersion
- Tooling damage
Solutions
Check whether the line is already visible on the free parison.
If the defect exists before moulding, investigate the extrusion system.
If the parison looks normal but the finished part has the defect, inspect:
- Mould surface
- Venting
- Air delivery
- Mould contamination
- Cavity condition
10. Rough or Poor Surface Finish
A rough surface can reduce the appearance and perceived quality of bottles, containers, tanks, and other plastic products.
Causes
- Incorrect melt temperature
- Moisture
- Poor mould venting
- Low blow air pressure
- Contaminated material
- Rough mould surface
- Unstable parison
- Poor material flow
Solutions
Check the defect from the outside inward:
- Inspect the mould surface.
- Check mould vents.
- Verify blow air delivery.
- Check melt temperature.
- Inspect the parison.
- Review material handling.
- Check for contamination.
Troubleshooting references identify moisture, air pressure, mould venting, and melt temperature among factors affecting rough surfaces.
11. Incomplete Blowing or Poor Mould Definition
The product does not completely reproduce the mould cavity.
You might see:
- Missing details
- Flattened sections
- Poor corners
- Incomplete handles
- Dull areas
- Incorrect shape
Possible causes
- Insufficient blow pressure
- Restricted blow air
- Blocked blow pin
- Poor mould venting
- Parison temperature too low
- Incorrect timing
- Air leakage
Solutions
Check the air path from the machine to the mould.
Then inspect:
- Blow pin
- Air pressure
- Air flow
- Blow timing
- Mould vents
- Parison temperature
- Mould temperature
A pressure reading at the compressor does not necessarily confirm adequate pressure and flow at the mould during the actual blow cycle.
12. Warpage and Dimensional Variation
Warpage becomes visible when the product changes shape after moulding or cooling.
Common causes
- Uneven cooling
- Blocked cooling channels
- Uneven wall thickness
- High melt temperature
- Early ejection
- Residual stress
- Uneven mould temperature
Solutions
Check:
- Cooling-water temperature
- Cooling-water flow
- Supply and return temperatures
- Cooling-channel condition
- Mould temperature distribution
- Cooling time
- Wall thickness distribution
Increasing cooling time might hide the problem temporarily. First confirm that the cooling system is working correctly.
13. Neck Deformation
Neck defects are especially important for bottles and containers because they can affect caps, closures, sealing, and filling operations.
Causes
- Mould or blow-pin misalignment
- Incorrect temperature
- Uneven cooling
- Trimming damage
- Excessive shrinkage
- Incorrect neck tooling
Solutions
Inspect:
- Neck dimensions
- Blow-pin alignment
- Mould alignment
- Cooling conditions
- Trimming process
- Neck tooling
Neck deformation and finish problems often require checking both the moulding process and downstream trimming operation.
14. Colour Variation and Poor Masterbatch Dispersion
Colour variation is another important blow moulding problem, especially for packaging, containers, tanks, automotive components, and consumer products.
Possible causes
- Incorrect masterbatch dosage
- Poor dispersion
- Incompatible carrier resin
- Incorrect mixing
- Material contamination
- Inconsistent feeding
- Excessive processing temperature
- Masterbatch batch variation
How to reduce colour-related defects
Use a masterbatch designed for the specific base polymer and application.
Check:
- Carrier compatibility
- Recommended let-down ratio
- Pigment concentration
- Processing temperature
- Dispersion quality
- Feeding accuracy
Surya Compounds & Masterbatches provides colour, black, white, additive, and application-specific masterbatch solutions for different polymer systems. Its masterbatch dosage guide also notes that the correct let-down ratio depends on pigment loading, opacity requirements, wall thickness, and the required additive concentration.
Read more: Masterbatch Dosage & Let-Down Ratio Guide
15. Poor UV Resistance and Outdoor Degradation
Some blow moulded products are exposed to sunlight for long periods.
Examples include:
- Water tanks
- Containers
- Agricultural products
- Outdoor storage products
- Automotive components
- Industrial packaging
Without suitable UV stabilization, plastic products can experience colour fading, chalking, brittleness, and loss of mechanical performance.
For outdoor blow moulding applications, evaluate the polymer, pigment, UV stabilizer, processing temperature, and expected exposure conditions together.
Surya Compounds & Masterbatches offers UV stabilizer masterbatch solutions for applications where resistance to outdoor UV exposure is required.
Read more: UV Stabilized vs UV Resistant Plastic
How to Troubleshoot Blow Moulding Defects Step by Step
When a defect appears, avoid changing several machine parameters at the same time.
Use this sequence.
Step 1: Identify the defect pattern
Ask:
- Does it appear in every part?
- Does it affect one cavity?
- Does it occur on one side?
- Does it appear randomly?
- Did it start after a material change?
- Did it start after maintenance?
Step 2: Inspect the material
Check:
- Resin grade
- Resin lot
- Regrind
- Masterbatch
- Additive dosage
- Material storage
- Moisture or condensation
- Material contamination
Step 3: Check the parison
Look for:
- Sagging
- Curling
- Thickness variation
- Surface roughness
- Die lines
- Colour streaks
- Unstable extrusion
Step 4: Check machine parameters
Review:
- Melt temperature
- Die-head temperature
- Extrusion speed
- Blow pressure
- Blow time
- Parison drop time
- Mould closing timing
These parameters are commonly involved in extrusion blow moulding troubleshooting.
Step 5: Inspect the mould
Check:
- Alignment
- Pinch-off
- Venting
- Cooling channels
- Cavity surface
- Blow pin
- Tool wear
Step 6: Change one variable at a time
Record the original setting.
Make one controlled change.
Run enough cycles to reach a stable condition.
Then compare:
- Part weight
- Wall thickness
- Dimensions
- Appearance
- Leakage
- Functional performance
This approach reduces trial-and-error and helps identify the real cause.
How Masterbatch Selection Affects Blow Moulding Quality
Masterbatch is more than a colour ingredient. Its carrier resin, pigment or additive system, dispersion quality, thermal stability, and dosage influence processing performance.
An unsuitable masterbatch can contribute to:
- Colour streaking
- Poor dispersion
- Surface defects
- Flow instability
- Plate-out
- Inconsistent colour
- Mechanical-property variation
The masterbatch carrier should be compatible with the base polymer and processing conditions. Surya’s MFI guide notes that carrier-flow compatibility helps maintain uniform dispersion and consistent processing.
For application-specific requirements, manufacturers should provide the base polymer, processing method, target colour, dosage, temperature range, end-use requirements, and relevant regulatory requirements to the masterbatch supplier.
Choosing Masterbatch for Blow Moulding Applications
Before selecting a masterbatch, define:
- Base polymer, such as HDPE, LDPE, PP or PET
- Blow moulding process
- Product type
- Desired colour
- Required opacity
- Outdoor or indoor application
- UV exposure
- Required mechanical properties
- Target dosage
- Food-contact or other regulatory requirements
- Recycling or regrind requirements
Surya Compounds & Masterbatches manufactures masterbatch and compound solutions for polymers including PVC, LLDPE, LDPE, HDPE, PP, PS, PET, TPU, HIPS, ABS, and EVA.
For PET bottle and container applications, see PET Masterbatch.
For applications where functional additives are required, see Silicone Additive Masterbatch.
Blow Moulding Defects: Material vs Machine vs Mould
A useful way to diagnose recurring problems is to classify them into four areas.
|
Area |
What to Check |
|
Material |
Resin grade, MFI, moisture, contamination, regrind |
|
Masterbatch |
Carrier compatibility, dosage, dispersion, thermal stability |
| Machine |
Temperature, extrusion, pressure, timing, alignment |
| Mould |
Pinch-off, venting, cooling, cavity surface, alignment |
This prevents teams from blaming the machine for every defect.
A material problem will not always disappear after changing machine settings. Similarly, a worn mould cannot always be corrected by changing melt temperature.
Preventing Blow Moulding Defects
Prevention starts with process control.
Use a documented production recipe covering:
- Resin grade
- Masterbatch grade
- Masterbatch dosage
- Processing temperatures
- Extrusion speed
- Blow pressure
- Blow time
- Parison programming
- Mould temperature
- Cooling conditions
- Target part weight
- Critical dimensions
Also maintain:
- Consistent raw material batches
- Clean feeding systems
- Regular die-head inspection
- Mould vent cleaning
- Cooling-channel maintenance
- Blow-pin inspection
- Accurate dosing equipment
- Regular quality checks
A stable process makes troubleshooting faster because the production team has a defined baseline.
Final Thoughts
Blow moulding defects usually have a traceable cause. The key is to identify whether the problem originates from material, masterbatch, parison formation, machine settings, mould condition, blowing air, or cooling.
Instead of making multiple adjustments at once, establish a stable baseline and troubleshoot one variable at a time.
For manufacturers, the right resin and masterbatch selection also matters. Compatibility, MFI, dispersion, dosage, thermal stability, and application requirements should all be considered before production.
Surya Compounds & Masterbatches supplies colour, black, white, additive, and compound solutions for different polymer processing applications. If you are facing recurring colour, dispersion, processing, or material-related problems, share your polymer grade, application, machine type, current masterbatch, dosage, and defect pattern with the technical team for application-specific guidance.
Explore Surya Compounds & Masterbatches for masterbatch and polymer compound solutions.
Frequently Asked Questions About Blow Moulding Defects
What are the most common blow moulding defects?
Common defects include uneven wall thickness, parison sagging, parison curling, excessive flash, weak pinch-off, blow-outs, bubbles, black specks, die lines, rough surfaces, incomplete blowing, warpage, neck deformation, leakage, and colour variation.
Why does blow moulding produce uneven wall thickness?
Uneven wall thickness often results from incorrect parison programming, die misalignment, uneven die-head temperature, parison sagging, incorrect mould positioning, or unsuitable material melt strength.
How do you fix parison sagging?
Start by checking melt temperature, resin melt strength, extrusion speed, parison length, and the time between extrusion and mould closing. Avoid changing several parameters simultaneously.
What causes excessive flash in blow moulding?
Excessive flash can result from excessive parison material, mould misalignment, poor mould closure, worn pinch-off areas, or incorrect parison positioning.
What causes black specks in blow moulded products?
Black specks are often associated with degraded polymer, contaminated regrind, foreign material, excessive residence time, overheating, or material trapped inside the extrusion system.
How do you prevent colour variation in blow moulding?
Use a compatible masterbatch, maintain accurate dosage, ensure consistent feeding, and verify pigment dispersion. The carrier resin should also be compatible with the base polymer.
Does MFI affect blow moulding?
Yes. MFI provides an indication of polymer flow behaviour. Blow moulding applications often require an appropriate balance between flow and melt strength. The correct MFI depends on the polymer, product design, equipment, and processing conditions.
How does moisture affect blow moulding?
Moisture or condensation can contribute to bubbles, streaks, surface problems, and inconsistent processing in susceptible materials. Follow the specific resin supplier’s handling and drying requirements.
How do you troubleshoot blow moulding problems?
Start by identifying the defect pattern. Then check the material, masterbatch, parison, machine settings, mould, air supply, and cooling system. Change one variable at a time and document the result.
Can masterbatch cause blow moulding defects?
Yes. An unsuitable carrier, poor dispersion, incorrect dosage, contamination, or inadequate thermal stability can contribute to colour, surface, flow, or processing problems.
