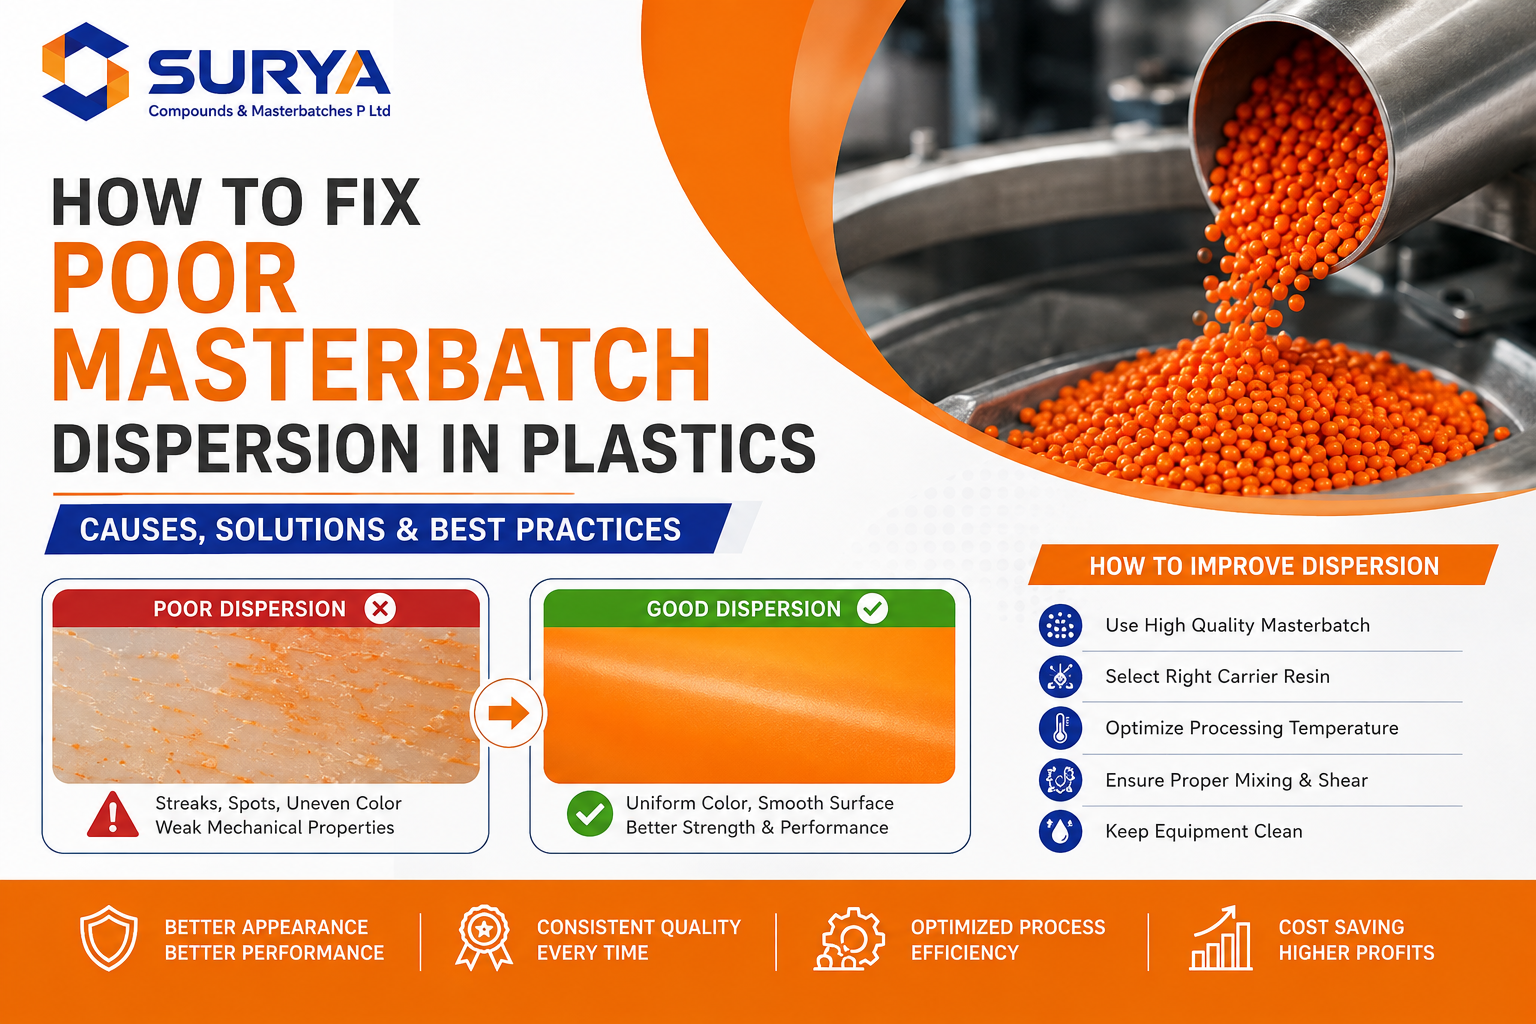
Poor masterbatch dispersion shows up as streaks, specks, uneven color, and weak spots in molded or extruded plastic. It happens when the pigment or additive carried in the masterbatch is not spread evenly and broken down finely enough in the melt. The result is wasted material, rejected parts, and unhappy customers. This guide explains what dispersion problems look like and why they happen and gives a step-by-step method to fix and prevent them.
| Quick answer: Poor masterbatch dispersion is usually caused by an incompatible carrier resin, too low a let-down ratio, insufficient melt mixing (low back pressure or screw shear), moisture, or agglomerated pigment. Fix it by matching the carrier to the base polymer, increasing back pressure and mixing, drying the material, correcting the dosage, and choosing a well-dispersed masterbatch. |
Why dispersion matters for quality and cost
Dispersion is not only a cosmetic concern. An agglomerate sitting in a thin film is a mechanical weak point that can tear or fail under stress, and in packaging it can cause pinholes that ruin barrier performance. Uneven color forces you to overdose masterbatch to hide the variation, which raises material cost on every part you make. Streaks and specks also increase scrap and slow the line as operators chase the fault. In short, good dispersion protects appearance, mechanical strength, and margin simultaneously, which is why it is worth diagnosing properly rather than masking with extra pigment.
What does poor dispersion look like?
Dispersion faults have a recognisable set of symptoms. Learning to read them tells you where to look:
- Colour streaks or swirls running along the direction of flow — the classic sign of uneven mixing.
- Specks or spots of concentrated pigment, which are agglomerates that were never broken down.
- Shade variation between one part and the next, or across a single part.
- Filter screen blockage or steadily rising melt pressure in an extrusion line.
- Weak points or pinholes in thin film, where an agglomerate sits and creates a flaw.
Distribution vs dispersion — the key difference
These two words are often used loosely, but separating them is the single most useful diagnostic step you can take. Distribution is how evenly the masterbatch is spread throughout the melt — a mixing problem. Dispersion is how well the pigment agglomerates are broken down into fine individual particles — a shear and formulation problem.
The symptom tells you which one you have. Streaks and swirls point to a distribution issue: the colour is present but not evenly mixed, so the fix lies in mixing energy and dosing. Specks and spots point to a dispersion issue: the pigment is there in lumps that never opened up, so the fix lies in shear, temperature and the quality of the masterbatch itself. Getting this diagnosis right saves hours of trial and error, because it steers you toward the correct group of causes below.
Common causes of poor masterbatch dispersion
|
Cause |
Why it happens | Typical symptom |
|
Incompatible carrier resin |
The carrier does not melt-blend with the base polymer | Streaks, poor mixing |
|
Let-down ratio too low |
Too little masterbatch to distribute evenly |
Streaking, weak colour |
|
Insufficient melt mixing |
Low back pressure or a low-shear screw | Uneven colour |
| Agglomerated pigment | Poorly dispersed masterbatch or damp pigment |
Specks, spots |
|
Moisture |
Wet masterbatch or hygroscopic resin |
Streaks, splay, voids |
| Processing temperature too low |
Carrier not fully melted |
Poor blending, specks |
| Worn or wrong screw design | Inadequate shear or mixing zones |
Persistent streaks |
The carrier resin deserves special attention, because it is the most common root cause and the easiest to overlook. If the carrier does not melt-blend cleanly with your base polymer — for example, a carrier with a very different melt flow or chemistry — no amount of mixing energy will fully homogenise it. Matching the carrier to the polymer is where most dispersion troubleshooting should begin.
How to fix poor dispersion — step by step
- Match the carrier resin to your base polymer — a PE-carrier masterbatch for PE, or a universal carrier verified for your polymer and process.
- Increase back pressure on the injection unit to improve melt homogenisation and work the material harder during recovery.
- Raise screw shear or mixing. Fit a mixing screw, a mixing nozzle or a static mixer for colours that are hard to disperse.
- Check and correct the let-down ratio. Raise it if you are under-dosing a very concentrated masterbatch that your mixing cannot spread evenly.
- Dry the material to the resin’s recommended moisture level, and add a desiccant masterbatch when running damp recyclate.
- Confirm the melt temperature is high enough to fully melt the carrier — but not so high that it degrades the pigment.
- Switch to a better-dispersed masterbatch made on a twin-screw line with high-quality pigment wetting if problems persist after the process changes.
How to prevent dispersion problems
Prevention is cheaper than firefighting. A few habits keep dispersion faults rare:
- Buy masterbatch with a carrier matched to your process and, where possible, a documented dispersion rating.
- Store masterbatch sealed and dry so it does not pick up moisture from the factory air.
- Use gravimetric dosing for consistent, repeatable addition from batch to batch.
- Run a filter or pressure test for film to catch agglomerates before they reach full production.
- Keep screws and mixing elements maintained so shear stays where it should be.
Frequently Asked Questions
What causes poor masterbatch dispersion?
The main causes are an incompatible carrier resin, a let-down ratio that is too low, insufficient melt mixing (low back pressure or low shear), pigment agglomeration, moisture, and processing temperatures too low to melt the carrier fully.
What is the difference between distribution and dispersion?
Distribution is how evenly the masterbatch is spread through the melt — a mixing issue that shows as streaks. Dispersion is how well pigment agglomerates are broken into fine particles — a shear and formulation issue that shows as specks.
How do I stop colour streaking in injection moulding?
Increase back pressure, use a mixing screw or nozzle, verify the carrier resin is compatible, correct the let-down ratio, and make sure the material is dry and the melt temperature is high enough to melt the carrier fully.
Can a better masterbatch fix dispersion issues?
Often, yes. A masterbatch made on a twin-screw line with well-wetted pigment and a carrier matched to your polymer disperses far more easily than a poorly compounded one, reducing both streaks and specks.
Does moisture affect dispersion?
Yes. Wet masterbatch or a hygroscopic base resin can cause streaks, splay and voids, and damp pigment tends to agglomerate. Dry the material to spec and store masterbatch sealed to avoid it.
